How to Choose a Ceramic Irregular Nozzle Manufacturer?
Choosing the right Ceramic Irregular Nozzle Manufacturer requires more than comparing prices or polished product photographs. Irregular nozzle geometry changes spray distribution, pressure loss, and wear behavior. Small dimensional errors can create visible coating bands, uneven cooling, or unstable material flow. The Global Advanced Ceramics Market report by Grand View Research highlights continuing demand for ceramics in high-temperature, wear-resistant applications. That trend matters because nozzle buyers increasingly expect measurable performance, not general claims.
Look for a manufacturer that understands your process. Ask whether it can control alumina, zirconia, or silicon carbide grades consistently. Request data for particle size, density, hardness, thermal shock resistance, and surface roughness. ISO 9001 certification can support process discipline, but certification alone proves little. The manufacturer should provide inspection records, batch traceability, and dimensional reports for critical openings. Ask for sample testing under your actual pressure, temperature, abrasive load, and fluid conditions. A laboratory report from ASTM-based testing is more useful than a brochure promise.
Be practical.
Reports from MarketsandMarkets and Allied Market Research also associate advanced ceramic growth with industrial automation, chemical processing, and energy equipment. These sectors demand repeatability and longer service life. Still, published market forecasts cannot predict your exact nozzle performance. I have seen technically impressive samples fail after installation because the mounting seat was overlooked. Therefore, evaluate engineering support, replacement consistency, lead time, and communication quality. The best Ceramic Irregular Nozzle Manufacturer should explain limitations clearly, document changes, and accept reasonable technical questions. A careful supplier may even challenge your initial design. That is often a good sign.
Define Nozzle Geometry, Spray Angle, Flow Rate, and Particle Size
How to Choose a Ceramic Irregular Nozzle Manufacturer?
Define Nozzle Geometry, Spray Angle, Flow Rate, and Particle Size
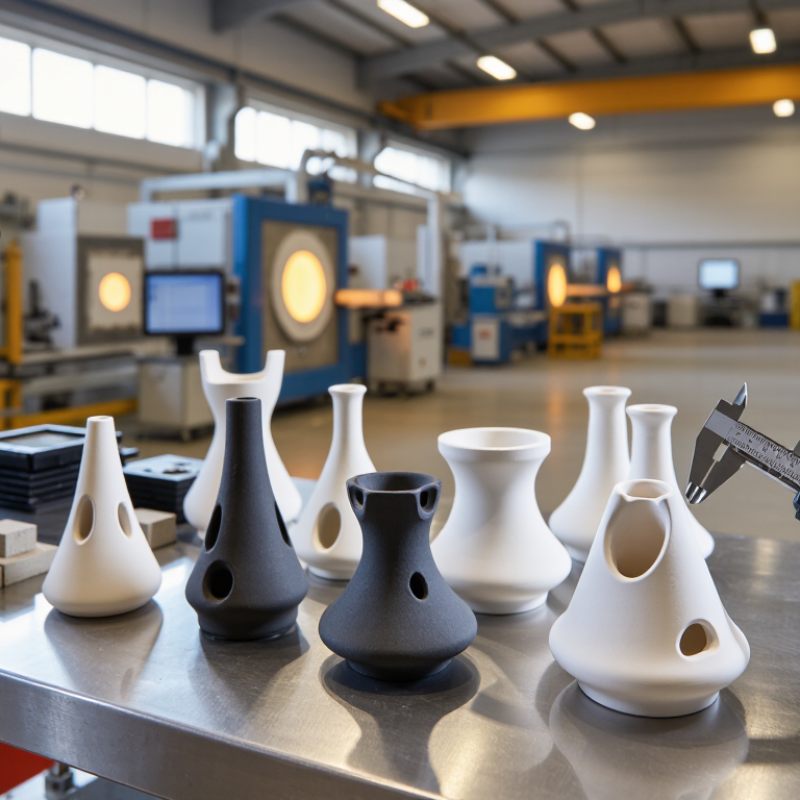
Choosing a ceramic irregular nozzle manufacturer starts with the part’s actual geometry. Request a dimensional drawing, including inlet shape, outlet profile, wall thickness, and mounting tolerance. Irregular nozzles can produce uneven patterns when the internal passage changes too sharply. Ask how the manufacturer controls these transitions during forming and firing. Measure twice.
Spray angle should match the working distance and target surface. A wider angle covers more area, but it may reduce impact intensity. Request spray-pattern images or test reports at several pressures. Flow rate must also be verified under specified conditions. Water temperature, pressure stability, and measurement equipment can change the result. A reliable supplier records these variables instead of offering one attractive number.
Particle size is equally important for process control. Ask whether the nozzle supports fine, medium, or coarse particles without frequent blockage. Examine the internal surface with magnification, especially near the narrowest passage. Dense ceramic may resist wear, but poor finishing can still disturb the spray. Sample testing is essential. Real testing can challenge a neat spreadsheet. Leave room for adjustment. A manufacturer with documented tolerances, repeatable samples, and clear inspection records is easier to evaluate professionally.
| Selection Dimension | Recommended Specification Range | What to Define | Why It Matters | Manufacturer Evaluation Point |
|---|---|---|---|---|
| Nozzle Geometry | Round, oval, slot, fan, multi-orifice, or custom irregular profile | Orifice length, width, aspect ratio, inlet radius, outlet profile, wall thickness, and mounting dimensions | Geometry controls spray distribution, impact pattern, pressure loss, and the risk of localized wear. | Request dimensioned drawings, coordinate tolerances, outlet-profile inspection, and sample-part approval before mass production. |
| Spray Pattern | Solid coneHollow coneFlat fanCustom | Target coverage shape, overlap requirement, spray uniformity, and allowable edge-loading | The correct pattern ensures even surface coverage and helps prevent streaks, dry zones, or excessive overspray. | Compare pattern images or distribution scans at the actual operating pressure and fluid viscosity. |
| Spray Angle | 15°–120° nominal, depending on geometry and pressure | Included spray angle at a defined pressure, stand-off distance, and liquid condition | A wider angle covers more area but generally reduces impact intensity at the same flow rate and distance. | Verify the angle at multiple pressures; the stated angle should not be treated as constant across the full operating range. |
| Liquid Flow Rate | Approximately 0.5–100 L/min per nozzle | Required flow at operating pressure, fluid temperature, density, viscosity, and specific gravity | Flow rate determines pump capacity, material consumption, coverage, and process throughput. | Ask for a pressure-versus-flow curve and a flow-rate tolerance, commonly expressed as a percentage of the nominal value. |
| Operating Pressure | Typically 1–20 bar; application-dependent | Minimum, nominal, and maximum pressure, including pressure fluctuations during operation | Pressure affects flow rate, spray angle, droplet formation, atomization, and wear rate. | Confirm pressure rating, hydrostatic test method, and performance data at the intended operating point. |
| Particle or Droplet Size | Approximately 50–1,000 µm for hydraulic spray; atomizing designs may be finer | Required droplet-size metric such as Dv10, Dv50, Dv90, or Sauter Mean Diameter | Particle size influences evaporation, penetration, drift, coating quality, filtration requirements, and environmental control. | Require the measurement method, instrument type, sampling position, liquid properties, and operating pressure used for testing. |
| Ceramic Material | Alumina, zirconia, silicon carbide, or other application-specific ceramic | Material grade, purity, density, hardness, fracture toughness, and chemical compatibility | Material selection affects abrasion resistance, thermal stability, corrosion resistance, and service life. | Check material certificates, batch traceability, sintering controls, and compatibility with the sprayed chemical or slurry. |
| Abrasive-Wear Resistance | Select high-hardness ceramic for slurries and suspended solids | Particle concentration, hardness, size distribution, velocity, and expected service hours | Abrasive media can enlarge the orifice and change flow rate and spray pattern over time. | Request comparative wear-test results using a representative slurry rather than relying only on a material hardness value. |
| Chemical Resistance | Must match pH, solvents, salts, oxidizers, and process temperature | Fluid composition, pH range, temperature, concentration, and exposure duration | Chemical attack can weaken the ceramic, affect mounting components, or change the internal flow surface. | Confirm compatibility for both the ceramic and any metal, elastomer, or adhesive used in the nozzle assembly. |
| Dimensional Tolerance | Critical orifice dimensions commonly controlled to approximately ±0.02–0.10 mm | Orifice size, profile accuracy, concentricity, flatness, mounting fit, and allowable variation between lots | Tight control improves interchangeability and keeps flow and spray-pattern variation within process limits. | Review inspection plans, calibrated measurement equipment, capability data, and a defined acceptance standard. |
| Surface Finish | Application-specific; smoother internal passages generally reduce turbulence and buildup | Internal roughness, polished areas, edge condition, chips, cracks, and glaze quality | Surface condition influences pressure loss, clogging tendency, particle retention, and repeatability. | Specify inspection criteria for the wetted passage and require visual or microscopic inspection of the outlet edge. |
| Clogging Control | Orifice passage typically sized according to the largest solids and filtration level | Maximum particle size, filter mesh, solids loading, flushing method, and clean-out frequency | An undersized orifice can cause frequent blockage, unstable flow, and unplanned maintenance. | Ensure the manufacturer provides a recommended filtration level and verifies passage continuity on every part. |
| Thermal Capability | Many technical ceramics tolerate high temperatures; assembly limits may be lower | Continuous temperature, thermal cycling, heating rate, cooling rate, and mounting stress | Thermal shock and uneven expansion can cause cracking even when the ceramic's nominal temperature limit is high. | Evaluate the complete nozzle assembly, including holder, seal, adhesive, and connection hardware. |
| Connection and Installation | Threaded, flanged, clamp-mounted, insert-style, or custom holder | Connection standard, sealing method, insertion depth, orientation, torque, and replacement procedure | Correct installation prevents leakage, misalignment, vibration damage, and accidental over-tightening. | Request installation instructions, recommended torque values, spare-part dimensions, and an alignment tolerance. |
| Quality Documentation | Inspection record and traceable batch documentation | Material certificate, dimensional report, flow test, pressure test, visual inspection, and lot identification | Documented controls make it easier to identify process drift and maintain consistent spray performance. | Prefer suppliers able to provide first-article inspection, production sampling plans, nonconformance control, and traceability. |
| Validation Testing | Prototype testing followed by pilot-lot verification | Actual fluid, pressure, temperature, stand-off distance, spray overlap, and operating cycle | Laboratory specifications may not predict performance with high-viscosity, abrasive, or chemically aggressive fluids. | Choose a manufacturer willing to produce samples, test under your process conditions, and document acceptance criteria. |