China Top Chocopie Cake Production Line Manufacturer?

Choosing the right China Top Chocopie Cake Production Line manufacturer requires more than comparing prices. It demands practical knowledge of cake formulation, equipment integration, hygiene control, and long-term service. A reliable supplier should connect mixing, baking, sandwiching, chocolate enrobing, cooling, inspection, and packaging into one stable process. Each stage affects the final product.

Zhang Wei, a confectionery automation engineer with experience in industrial snack production, says, “A good Chocopie Cake Production Line must protect product consistency before it increases output.” This view is important for buyers evaluating Chinese manufacturers. A modern line should maintain accurate batter weight, even cream distribution, and controlled chocolate temperature. Cooling tunnels need steady airflow. Packaging machines must handle soft cakes without damaging their edges.

Details reveal manufacturing quality. Stainless-steel contact parts should be easy to clean. Servo-driven systems can improve filling accuracy. Sensors should detect missing cakes, broken wrappers, and temperature changes. The manufacturer should also provide installation guidance, operator training, spare parts, and production testing before shipment.

High speed alone is not enough.

Some suppliers present impressive capacity figures, yet practical output may fall below expectations. Product size, chocolate thickness, factory humidity, and worker skill can change results. Buyers should request sample production, equipment videos, layout drawings, and clear energy data. They should also examine after-sales response times.

No production line is perfect. Even experienced factories must adjust recipes, cooling time, and packaging settings. That honest evaluation can prevent expensive mistakes. The best manufacturer is not simply the cheapest option. It is the partner that offers dependable engineering, measurable performance, and room for future improvement.

China Top Chocopie Cake Production Line Manufacturer?

China’s Leading Chocopie Cake Production Line Manufacturer

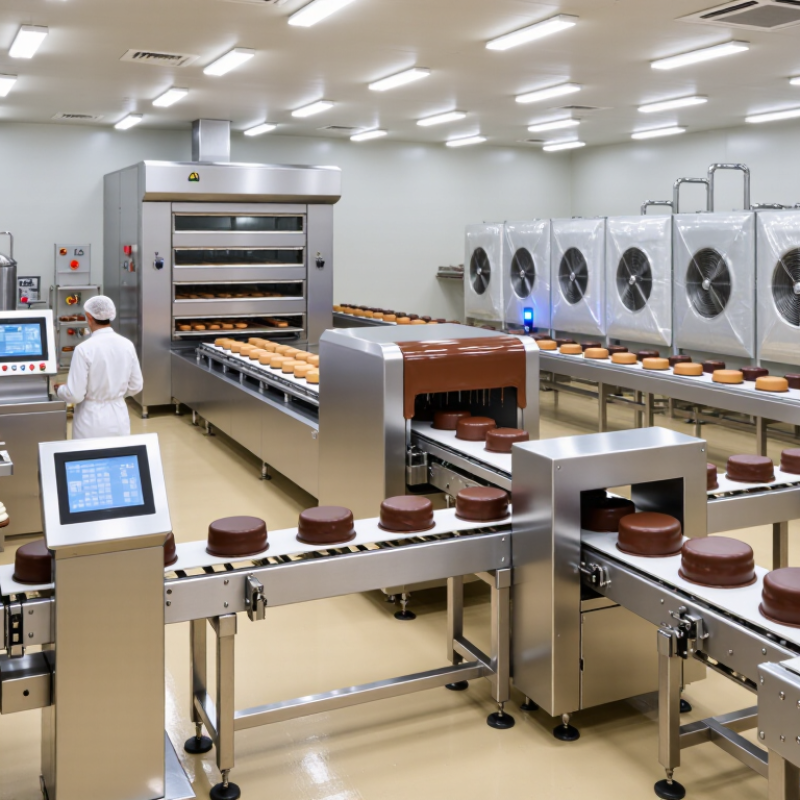
China’s leading Chocopie cake production line manufacturer combines practical engineering with reliable food-processing knowledge. Its production systems support mixing, depositing, baking, cooling, filling, coating, and automatic packaging. Each stage must stay synchronized. A small temperature error can change cake softness and filling stability.

Experienced engineers normally select stainless-steel structures, food-grade contact parts, and easy-clean conveyor designs. They also adjust baking temperature, belt speed, and filling volume for different recipes. Clear control panels help operators monitor production without unnecessary complexity. Production data, inspection records, and traceable components improve confidence during installation and daily operation.

A dependable manufacturer should provide testing before shipment, operator training, and responsive technical support. Factory acceptance testing can reveal uneven coating or unstable cooling early. No line is perfect.

Real projects often need adjustment. Humidity, local ingredients, and factory space can affect performance. A responsible supplier studies these details instead of offering a fixed solution. It may recommend pilot tests, revised molds, or slower initial production. This approach requires more time, but it reduces waste and protects product consistency. Reliable equipment is not only about speed; it is about stable cakes, clean operation, and measurable results over years of use.

Chocopie Cake Production Line Design and Manufacturing Process

China Top Chocopie Cake Production Line Manufacturer?

Designing a chocopie cake production line starts with the recipe, not the machine list. Cake density, filling viscosity, and coating temperature shape every engineering decision. Experienced engineers test batter flow before selecting depositors. They also measure baking loss, moisture migration, and product thickness. Small changes matter. A soft center needs controlled cooling. Otherwise, the filling may spread during enrobing. The line should include mixing, depositing, baking, cooling, filling, coating, setting, and packing sections.

A practical design uses stainless steel food-contact surfaces and accessible cleaning points. Servo-driven depositors improve portion accuracy and reduce material waste. Tunnel ovens need stable airflow, accurate temperature zones, and reliable belt tracking. Cooling conveyors require enough residence time for the cake structure to settle. Chocolate coating systems should control viscosity continuously. Temperature fluctuations create dull surfaces or uneven coverage. That problem is common.

Manufacturing should follow approved drawings, component checks, assembly records, and factory acceptance tests. A dependable manufacturer verifies electrical safety, guarding, sanitation, and emergency stops before shipment. Trial production with the customer’s actual recipe is strongly recommended. It exposes weak points early. The first layout is rarely perfect. Operators may need wider access doors, clearer controls, or simpler changeover tools. These details often decide whether a line performs well after installation. Performance data, maintenance instructions, spare-parts lists, and operator training should accompany the equipment. Reliable support continues after commissioning.

Chocopie Cake Production Line Design and Manufacturing Process

The chart presents typical industrial processing temperatures used in a continuous chocopie cake production line. Baking is performed at a higher temperature, while chocolate coating and cooling require controlled lower-temperature conditions to protect product texture, coating quality, and packaging stability.

Core Equipment Used in Chocopie Cake Production

China Top Chocopie Cake Production Line Manufacturer?

A reliable chocopie cake line starts with accurate batter preparation. Industrial mixers blend flour, eggs, sugar, oil, and leavening agents at controlled speeds. The depositing machine then places equal portions onto baking trays. Weight variation affects cake thickness and filling alignment. Small errors become obvious later.

The tunnel oven is the core baking unit. It uses several temperature zones to control surface color, moisture, and internal structure. Experienced operators adjust belt speed after checking real cake samples, not only screen data. Cooling conveyors reduce product temperature before cream injection. The sandwiching unit applies a measured cream layer between two cake pieces. Hygienic design matters here. Smooth stainless-steel surfaces reduce residue and simplify cleaning.

The chocolate enrobing machine covers each cake evenly. A curtain of melted coating must maintain stable temperature and flow. A cooling tunnel then sets the shell without dull patches or cracks. Automatic packaging equipment seals individual pieces and protects them from humidity. Metal detection and weight checks support consistent quality control. Production records should include oven settings, filling weight, coating temperature, and cleaning times. No line is perfect. Thick cream, uneven cakes, and seasonal humidity can still challenge operators. A careful manufacturer should provide trial production, training, and documented acceptance checks before installation.

Quality Control and Food Safety Standards

China Top Chocopie Cake Production Line Manufacturer?

Quality Control and Food Safety Standards

A dependable chocopie line begins with hazard analysis, not glossy machinery. Engineers should map mixing, baking, cooling, filling, coating, and packing. Each step needs a measurable control. Codex CXC 1-1969, revised in 2022, recommends HACCP-based preventive controls. For soft cakes, teams should verify oven profiles, core temperature, water activity, and cooling time. These details expose risks that a fast visual inspection can miss.

No line is perfect.

On the factory floor, operators should record batch temperatures electronically and challenge metal detectors with validated test pieces. Sanitation teams need pre-operational checks, allergen changeover records, and environmental swabs around conveyors and cooling tunnels.

A practical supplier should provide calibration certificates, traceability exercises, and corrective-action records, not just a compliance folder. WHO estimates that unsafe food causes 600 million illnesses and 420,000 deaths worldwide each year (WHO, Estimates of the Global Burden of Foodborne Diseases, 2015). FDA 21 CFR Part 117 also emphasizes hazard analysis, preventive controls, monitoring, and verification.

Yet paperwork can become performative. Managers should test whether workers can explain a failed reading and contain affected product. That uncomfortable drill often reveals the real weakness.

Reliable acceptance testing should include product samples, line-speed trials, seal checks, and documented release criteria.

How to Select a Reliable Chocopie Production Line Manufacturer

China Top Chocopie Cake Production Line Manufacturer?

How to Select a Reliable Chocopie Production Line Manufacturer

Selecting a chocopie production line manufacturer requires more than comparing prices. In factory evaluations, I have learned that stable forming, baking, cooling, and coating matter most. Ask for complete process drawings and hourly output data. Confirm whether the line handles your recipe, filling weight, and cake dimensions. A reliable supplier should explain temperature zones, conveyor speeds, and cleaning access clearly. Vague answers deserve caution.

Tips: Request a test run with your ingredients. Check the cake’s height, filling position, coating thickness, and breakage rate. Visit an operating factory if possible. Speak with current users about maintenance response and spare-part delivery. Review electrical standards, safety protection, installation support, and operator training before signing any agreement. Small details matter.

Do not judge quality from polished videos alone. I once underestimated cooling time, and the coating later cracked during packaging. That experience changed my evaluation process. Ask for factory acceptance testing and site acceptance testing requirements in writing. Inspect stainless-steel contact parts, sensor brands, guarding, and emergency-stop locations. The manufacturer should provide manuals, component lists, service records, and a realistic production schedule. Independent inspection can also reveal alignment problems or incomplete documentation. A dependable partner welcomes difficult questions, even when the answer is not perfect.

China Top Chocopie Cake Production Line Manufacturer? - How to Select a Reliable Chocopie Production Line Manufacturer

Technical and purchasing criteria for evaluating a reliable Chocopie cake production line manufacturer

Selection Dimension Typical Industry Reference What a Reliable Manufacturer Should Provide Recommended Verification Method
Production Capacity Approximately 1,000–10,000 pieces per hour, depending on cake size, filling quantity, and line configuration. Clearly defined output based on a specified product recipe, piece weight, and operating speed. Request a factory acceptance test using the buyer’s actual product formula and target piece weight.
Product Size and Weight Common small snack-cake formats are generally produced within a broad range of approximately 20–80 g per piece. Adjustable depositing, sandwiching, cutting, and coating systems that match the required product dimensions. Check sample products, dimensional tolerance, weight deviation, and changeover procedure.
Process Configuration A complete line may include batter preparation, depositing, baking, cooling, cream filling, chocolate coating, cooling, and packaging. A process flow diagram, equipment list, utility requirements, and clearly stated scope of supply. Compare the proposed line layout with the actual recipe and confirm which operations are manual or automatic.
Baking System Industrial cake baking commonly uses controlled tunnel-oven zones, with temperature settings selected according to batter composition and product thickness. Independent temperature control by zone, stable conveyor speed, insulation, exhaust control, and accessible maintenance points. Review temperature uniformity records and test the cake’s moisture, color, texture, and internal doneness.
Cooling System Cooling time varies with cake thickness, recipe, ambient conditions, and the required filling or coating temperature. A hygienic cooling conveyor with controlled airflow and sufficient residence time before filling and chocolate coating. Confirm that the product reaches the required core temperature without excessive drying or deformation.
Filling Accuracy Typical cream or filling quantity is determined by product design and is often controlled through a metering pump or depositing system. Stable filling pressure, adjustable dosing, easy cleaning, and protection against air pockets or uneven distribution. Measure filling-weight variation across multiple production batches and inspect the sandwich alignment.
Chocolate Coating Coating systems generally include a chocolate tank, circulation or tempering function, enrobing curtain, vibration section, and cooling tunnel. Accurate chocolate-temperature control, adjustable coating thickness, stable circulation, and cleanable food-contact surfaces. Test coating weight, surface appearance, adhesion, setting time, and product temperature after cooling.
Packaging Compatibility Common options include individual film wrapping, flow wrapping, tray packing, carton packing, or combinations of these systems. Packaging equipment matched to product dimensions, film type, sealing requirements, production speed, and date-coding needs. Run the intended packaging material and verify seal strength, seal integrity, alignment, and package appearance.
Food-Contact Materials Stainless steel is widely used for food-contact parts because it is durable, cleanable, and resistant to corrosion. Material specifications, food-contact declarations, hygienic welds, accessible surfaces, and documented component information. Inspect material certificates, weld quality, surface finish, and cleaning accessibility before purchase.
Electrical and Control System Modern lines commonly use PLC-based control, touchscreen operation, variable-frequency drives, sensors, and safety interlocks. Electrical drawings, control logic, alarm records, recipe storage, multilingual interface options, and backup procedures. Test emergency stops, guards, alarms, sensor functions, data backup, and operator access levels.
Energy and Utility Requirements Utilities may include electricity, compressed air, water, ventilation, refrigeration, and gas or electric heating, depending on the design. A complete utility consumption estimate based on rated production capacity and operating conditions. Compare connected load with actual consumption data from a production test and confirm factory utility availability.
Hygiene and Cleaning Food machinery should minimize product-contact dead zones and allow routine cleaning, inspection, and sanitation. Tool-free or quick-release components where practical, drainage provisions, cleaning instructions, and sanitation schedules. Perform a cleaning demonstration and inspect conveyors, pumps, nozzles, tanks, corners, and product-contact areas.
Safety Compliance Industrial machinery should incorporate guarding, emergency stops, electrical protection, and risk-reduction measures appropriate to the installation. A documented risk assessment, safety circuit description, guarding design, and compliance documentation for the destination market. Review technical files, safety test records, manuals, and conformity documents before shipment.
Installation and Commissioning Complex food-production lines normally require professional installation, alignment, calibration, and operator training. Detailed installation drawings, commissioning procedures, training plans, and clearly defined customer responsibilities. Include installation milestones, acceptance criteria, travel costs, and commissioning duration in the contract.
Spare Parts Availability Wear parts may include belts, seals, heaters, sensors, pumps, cutting components, and electrical control parts. A recommended spare-parts list, part numbers, lead times, prices, and an after-sales contact channel. Confirm availability of critical parts and request a minimum spare-parts package for initial operation.
Warranty and Technical Support Warranty terms vary by supplier and should specify coverage, exclusions, response time, and service method. Written warranty conditions, remote troubleshooting, software support, service response targets, and optional maintenance plans. Evaluate the service agreement separately from the equipment quotation and obtain support escalation contacts.
Factory Testing and Acceptance Factory acceptance testing helps verify capacity, product quality, controls, safety functions, and packaging performance before shipment. A documented FAT protocol with measurable pass/fail criteria and test records. Use approved samples, recipes, packaging materials, and inspection checklists during the acceptance test.
Documentation Quality Complete documentation should cover operation, maintenance, electrical systems, spare parts, safety, and cleaning. English manuals, as-built drawings, wiring diagrams, software backups, maintenance schedules, and component lists. Make delivery of complete documentation a contractual requirement before final payment.
Total Cost of Ownership Purchase price is only one part of the cost; energy, labor, waste, maintenance, spare parts, and downtime also affect long-term value. A transparent quotation that separates equipment, installation, training, packaging integration, utilities, shipping, and optional items. Compare five-year operating costs rather than evaluating suppliers only by initial purchase price.
Supplier Reliability Reliable project delivery depends on engineering capability, production resources, quality control, and documented after-sales processes. References for comparable projects, project schedule, quality-control procedures, and evidence of successful commissioning. Visit the manufacturing site when possible and speak with previous customers about uptime and service performance.
Overall Selection Recommendation Best Value: Verified Performance Select the manufacturer that can demonstrate stable product quality, transparent specifications, hygienic design, effective support, and measurable acceptance results. Use a weighted scorecard covering capacity, quality, safety, service, delivery, operating cost, and total project risk.
Note: The technical ranges shown above are general industry reference values rather than guarantees for a specific production line. Final performance depends on the recipe, product size, filling, chocolate coating, packaging material, plant conditions, and validated operating parameters.
Scroll to Top